ARTICLE · 1324670
HOW TO WRITE A WPS AS PER ASME SECTION IX? 如何按照ASME第IX卷编写?
🔍 HOW TO WRITE A WPS AS PER ASME SECTION IX?
🔍 如何按照ASME第IX卷编写WPS?
A Welding Procedure Specification (WPS) is one of the most important documents in welding quality management
焊接工艺规程(WPS)是焊接质量管理中最重要的文件之一
It defines how welding must be performed to achieve the required weld quality, mechanical properties and compliance with applicable codes and project specifications.
它规定了必须如何执行焊接,以达到所需的焊缝质量、力学性能,并符合适用规范和项目规格。
📘 Key areas to understand when preparing or reviewing a WPS:
📘 在编制或审查WPS时需要理解的关键领域:
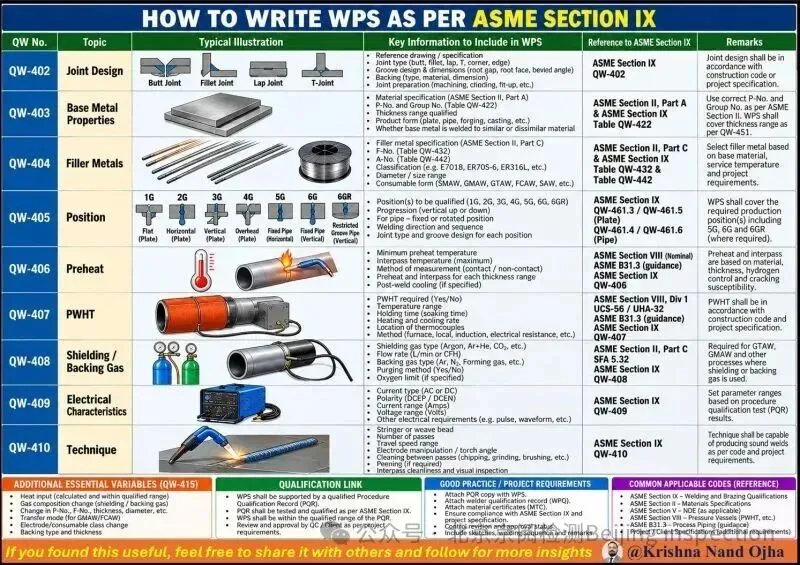
🔹 QW-402 – Joint DesignJoint type, groove design, root opening, root face, groove angle, backing and joint preparation requirements.
🔹 QW-402 – 接头设计:接头类型、坡口设计、根部间隙、钝边、坡口角度、衬垫和接头制备要求。
🔹 QW-403 – Base MetalsMaterial specifications, P-Numbers, Group Numbers where applicable, thickness ranges and qualified material combinations.
🔹 QW-403 – 母材:材料规格、P编号、适用时的组号、厚度范围以及已评定的材料组合。
🔹 QW-404 – Filler MetalsFiller metal classification, F-Number, A-Number where applicable, diameter, deposited weld metal thickness and other applicable variables.
🔹 QW-404 – 填充金属:填充金属分类、F编号、适用时的A编号、直径、熔敷焊缝金属厚度及其他适用变量。
🔹 QW-405 – Welding PositionsWelding position and progression requirements, including 1G, 2G, 3G, 4G, 5G, 6G and 6GR where relevant. Remember that position qualification depends on the applicable code rules and qualification test performed.
🔹 QW-405 – 焊接位置:焊接位置和焊接方向要求,包括相关情况下的1G、2G、3G、4G、5G、6G和6GR。请记住,位置评定取决于适用规范规则和所进行的评定试验。
🔹 QW-406 – Preheat and Interpass TemperatureMinimum preheat, maximum interpass temperature where specified, and temperature control to help prevent cracking and maintain required material properties.
🔹 QW-406 – 预热和层间温度:规定的最低预热温度、最高层间温度(如规定),以及有助于防止开裂并保持所需材料性能的温度控制。
🔹 QW-407 – Post Weld Heat Treatment (PWHT)Applicable heat-treatment condition, temperature range, holding time and other requirements established by the governing code and project specification.
🔹 QW-407 – 焊后热处理(PWHT):适用的热处理条件、温度范围、保温时间以及由 governing code 和项目规格确定的其他要求。
🔹 QW-408 – Shielding and Backing GasGas composition, shielding arrangements, backing gas and purging requirements, particularly for stainless steel, duplex and corrosion-resistant alloy welding.
🔹 QW-408 – 保护气和背面保护气:气体成分、保护布置、背面保护气和吹扫要求, particularly 用于不锈钢、双相钢和耐腐蚀合金焊接。
🔹 QW-409 – Electrical CharacteristicsCurrent type, polarity, amperage, voltage, heat input and other applicable electrical variables.
🔹 QW-409 – 电气特性:电流类型、极性、电流、电压、热输入及其他适用电气变量。
🔹 QW-410 – Welding TechniqueStringer or weave beads, number of passes, travel speed, cleaning between passes, back-gouging, electrode manipulation and other applicable technique variables.
🔹 QW-410 – 焊接技术:直线焊道或摆动焊道、道数、行走速度、道间清理、背面清根、焊条操作及其他适用技术变量。
📌 Additional points every QA/QC professional should verify:
📌 每位QA/QC专业人员都应核实的附加要点:
✅ The WPS is supported by an appropriate, qualified PQR where required
✅ 在需要时,WPS由适当且合格的PQR支持
✅ Essential variables & supplementary essential variables when impact toughness requirements apply, are correctly identified & controlled
✅ 当适用冲击韧性要求时,正确识别和控制重要变量及补充重要变量
✅ The proposed WPS falls within the qualification ranges established by ASME Section IX
✅ 拟采用的WPS处于ASME第IX卷所建立的评定范围内
✅ Welder performance qualification is verified separately from procedure qualification
✅ 焊工技能评定与工艺评定分开核实
✅ Material traceability, consumable control, preheat, interpass temperature, PWHT & inspection requirements are addressed
✅ 材料可追溯性、焊材控制、预热、层间温度、PWHT和检验要求均已涵盖
✅ The applicable construction code, client specifications & project requirements are followed alongside ASME Section IX
✅ 在遵循ASME第IX卷的同时,遵守适用的建造规范、客户规格和项目要求